
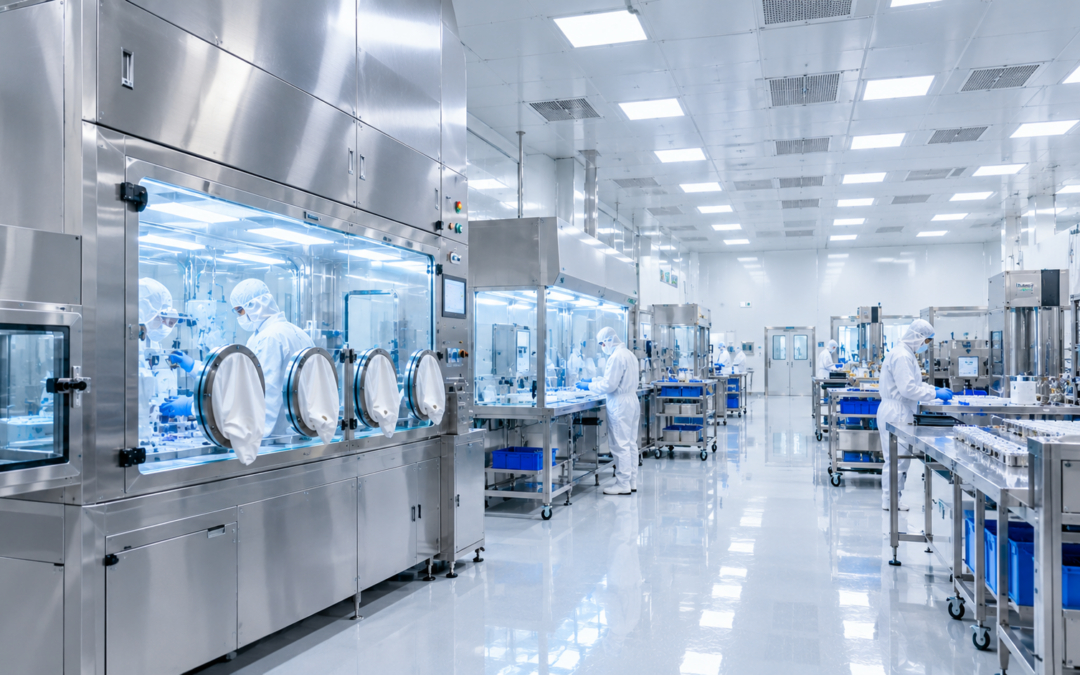
Selecting the right cleanroom equipment supplier is a strategic decision that extends well beyond price comparison. In regulated industries – pharmaceutical manufacturing, biotech, medical devices, microelectronics – the equipment installed in a cleanroom directly affects product quality, patient safety, and regulatory compliance. A wrong choice can result in qualification failures, costly retrofits, or facility shutdowns during inspections.
The European cleanroom market offers a range of suppliers, from large catalogue distributors to specialised manufacturers with direct engineering capability. Understanding what distinguishes a reliable partner from a generic vendor requires looking at specific criteria: regulatory alignment, technical competence, customisation depth, and the quality of long-term support. This article outlines the factors that procurement and engineering teams should evaluate when sourcing cleanroom equipment in Europe.
Why Choosing a European Cleanroom Equipment Supplier Has Regulatory Advantages
Working with a cleanroom equipment supplier based in Europe carries measurable regulatory advantages for facilities operating under EU GMP, ISO 14644, or national health authority frameworks.
European manufacturers are required to design and certify equipment in accordance with EU machinery directives, pressure equipment directives, and electromagnetic compatibility regulations. This means CE marking is not simply a label — it reflects a documented conformity assessment process that includes technical file compilation, risk analysis, and, for certain equipment categories, third-party notified body review. For pharmaceutical and biotech facilities subject to GMP audits, equipment supplied with full CE documentation simplifies the qualification process and reduces the risk of regulatory findings related to equipment provenance.
Beyond documentation, proximity matters operationally. A European supplier shares the same regulatory reference framework as the end user. When EU GMP Annex 1 (2022) introduces updated requirements for contamination control strategy, or when ISO 14644-3 guidance on testing methods is revised, a European manufacturer absorbs and incorporates these changes directly into its product development cycle. The same cannot always be assumed of suppliers based outside the EU, where regulatory alignment may require explicit verification and documentation effort on the buyer’s side.
Language, time zone alignment, and direct access to the manufacturer’s engineering team are additional practical factors. During qualification phases – IQ, OQ, PQ – rapid access to documentation, test data, and technical clarification can determine whether a project stays on schedule.
CE Marking, ISO Compliance, and Local Support from a European Cleanroom Supplier
CE marking and ISO compliance are minimum requirements when sourcing cleanroom equipment in Europe, but their depth varies significantly between suppliers.
CE marking must be verified for each equipment category. An air shower, an isolator, a pass box, and a fan filter unit each fall under different EU directives, and compliance documentation must be specific to the product model and configuration supplied. Buyers should request the full Declaration of Conformity for each unit, along with the technical file reference number, to confirm that certification covers the actual purchased configuration — not a generic family declaration.
ISO compliance in the context of cleanroom equipment refers to several distinct standards:
- ISO 14644-1: particle concentration limits and cleanroom classification
- ISO 14644-3: test methods for cleanroom performance verification
- ISO 14644-4: design and construction guidance
- EN ISO 29463: efficiency testing of HEPA and ULPA filters
A supplier that understands these standards at a technical level – not merely as checkboxes – is better positioned to support validation. This distinction becomes apparent when the buyer requests filter test certificates, airflow uniformity data, or particle count results at the filter face: a qualified supplier provides these as standard; a less rigorous one may be unable to produce them on request.
Local support infrastructure is the third pillar. Equipment installed in a cleanroom requires periodic maintenance, filter replacement, and performance requalification. A European supplier with a local technical service network – or with direct engineering staff available for on-site support – reduces response time when issues arise and simplifies the logistics of scheduled maintenance.
Technical Customisation vs Off-the-Shelf Solutions from Your Cleanroom Equipment Partner
Many cleanroom procurement decisions begin with a standard product catalogue, but regulated environments rarely fit standard configurations. Room dimensions, process constraints, pressure differential requirements, integration with monitoring systems, and specific regulatory expectations all create the need for equipment that departs from catalogue specifications.
The ability of a European cleanroom equipment supplier to deliver genuine technical customisation — not superficial modifications — is a differentiating factor that directly affects project outcome.
Technical customisation in cleanroom equipment typically covers:
- Dimensional adaptation: housing dimensions modified to fit non-standard ceiling grids, wall openings, or transfer apertures
- Material specification: choice between AISI 304 and AISI 316L stainless steel, surface finish selection (satin scotch-brite, electropolished), and seal material selection based on chemical compatibility
- Filtration configuration: HEPA H14 or ULPA filter grades, filter count, airflow velocity targets, and integrated monitoring ports
- Control and interlock systems: mechanical vs electromagnetic interlocks, touch panel interfaces, Modbus or BACnet integration, EWON Flexy remote access, data logging outputs for GMP audit trails
- Pressure regime: positive or negative pressure configurations for isolators, with validated airflow cascade management
Off-the-shelf solutions have a legitimate role in lower-risk areas – ancillary support zones, ISO Class 7 to 8 environments, or non-GMP laboratory settings – where standard performance profiles are sufficient. For Grade A/B environments, ATMP production, cytotoxic drug compounding, or any area subject to regulatory inspection with equipment-specific audit requirements, custom-engineered solutions reduce qualification risk and deliver better long-term performance.
The key question to ask any prospective cleanroom equipment supplier is not whether they offer customisation, but whether their engineering team can develop and document a custom solution to the buyer’s User Requirements Specification — and provide the technical drawings, test reports, and qualification documentation to support it through IQ/OQ.
Lead Time, After-Sales Service, and Spare Parts Availability
Lead time is often underweighted in cleanroom equipment procurement decisions, particularly during facility construction phases where schedules are compressed. A supplier that quotes competitive pricing but operates on extended delivery timelines – or that subcontracts manufacturing across multiple regions – introduces schedule risk that can cascade through the project.
European cleanroom equipment manufacturers with in-house fabrication capability typically offer more predictable and shorter lead times than distributors importing from outside the EU. Direct control over the manufacturing process allows schedule adjustments in response to project urgency and reduces exposure to customs delays, shipping disruptions, or quality control issues at the point of import.
After-sales service is a longer-term consideration that carries operational and regulatory weight. GMP-regulated facilities are required to maintain equipment in a validated state throughout its operational life. This means:
- Scheduled maintenance must be performed and documented
- Filter replacements must use approved components with traceable certification
- Any modification to equipment configuration requires change control and, in many cases, partial requalification
A cleanroom equipment supplier that provides a structured maintenance programme, supplies certified spare parts, and maintains documentation records compatible with GMP audit requirements is a significantly more valuable partner than one that ends its involvement at delivery.
Spare parts availability is particularly relevant for long-lifecycle equipment such as isolators, pass boxes, and air shower systems. Key components – ECM motors, HEPA filter cassettes, interlock actuators, seals, and control modules – should be available from the supplier with defined lead times and with part numbers referenced in the equipment documentation.
Why AGMM TECH Is a Trusted European Cleanroom Equipment Supplier
AGMM TECH is a European manufacturer of cleanroom equipment with direct engineering and fabrication capability. Its product range covers fan filter units, laminar flow hoods, positive and negative pressure isolators, static and dynamic pass boxes, air showers, softwall cleanroom enclosures, and cleanroom furniture, all designed and manufactured in-house in accordance with EU GMP, ISO 14644, and CE marking requirements.
Equipment is fabricated in AISI 304 stainless steel with TIG-welded construction and satin scotch-brite surface finish as standard. HEPA H14 filtration is standard across product lines; ULPA is available on request. Control systems are configurable with touch panel interfaces, Modbus TCP integration, and EWON Flexy remote monitoring for facilities requiring data logging and remote access during operation.
AGMM TECH works directly with engineering and procurement teams to develop custom configurations from User Requirements Specification documents, providing technical drawings, filter test certificates, CE Declarations of Conformity, and IQ/OQ documentation packages as part of the standard project deliverable set.
For facilities evaluating cleanroom equipment suppliers in Europe, AGMM TECH is available to provide technical consultation, product specifications, and project-specific documentation to support the qualification and procurement process.
Conclusion
Choosing a cleanroom equipment supplier in Europe is not a purely commercial decision — it is a technical and regulatory commitment that will shape the performance, compliance record, and operational continuity of a facility for years. The difference between a reliable European manufacturer and a generic distributor becomes visible not at the point of purchase, but during qualification, routine maintenance, and regulatory inspection.
The criteria outlined in this article – regulatory alignment, CE documentation depth, genuine customisation capability, predictable lead times, and structured after-sales support – provide a practical framework for evaluating prospective suppliers before committing to a project. Each of these dimensions carries a different weight depending on the application: a Grade A aseptic manufacturing environment demands more rigorous supplier qualification than an ISO Class 7 support area, while an ATMP production facility places greater emphasis on interlock documentation and pressure regime validation than a standard pharmaceutical packaging line.
What remains constant across all regulated environments is the need for a supplier who understands the regulatory context of the buyer, speaks the same technical language, and can provide the documentation that connects equipment specifications to qualification evidence. In Europe, this alignment is more naturally available from a manufacturer operating within the same regulatory framework – one that follows EU GMP guidance, complies with CE marking directives, and designs products with ISO 14644 as a structural reference rather than an afterthought.
For engineering and procurement teams currently evaluating cleanroom equipment suppliers, AGMM TECH is available to provide technical specifications, custom configuration proposals, and documentation packages tailored to the qualification requirements of each project. Direct contact with the engineering team is the most efficient way to assess whether a supplier’s capabilities match the specific demands of a facility.


